
Functions
Welcome to the page dedicated to the features of the equipment designed and manufactured by SINEX. Whether you operate in the food industry, waste recycling, pharmaceuticals, the chemical industry, or any other industrial sector, our equipment is tailored to meet your specific needs.We are committed to delivering custom solutions to optimize your industrial processes, regardless of your field of activity.
Search by Functions
You can refine your product search by selecting multiple functions to find the machine that best suits your needs.
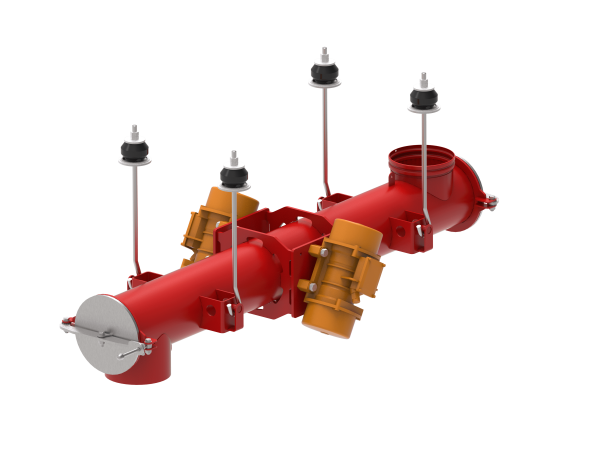
Electromechanical Vibrating Tubular Conveyor
Vibration conveying limits abrasion, prevents the creation of fines (no mechanical constraints on the product), and ensures a constant and controlled volumetric flow.
Suitable for extraction under silos, dosing, or transfer up to 8 meters, the vibrating tubular conveyor is the sealed solution ideal for all bulk handling industries.
Maintenance is facilitated by the absence of moving parts in contact with the product, as well as the use of reliable motorization (vibrating motors or magnetic bases) ensuring maximum availability.
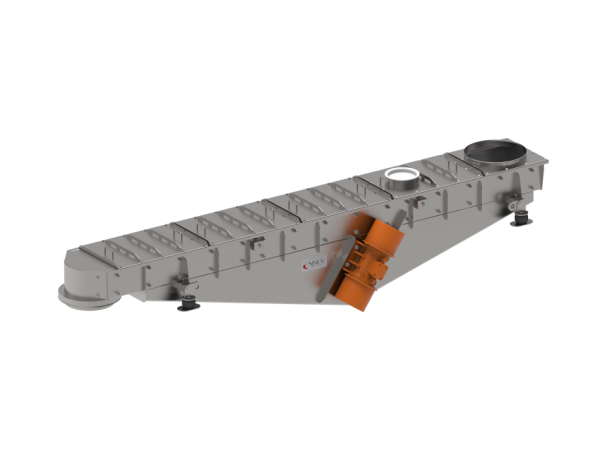
Electromechanical Rectangular Vibrating Conveyor
Vibration conveying limits abrasion, prevents the creation of fines (no mechanical constraints on the product), and ensures a constant and controlled volumetric flow. This vibratory conveying technology is particularly suitable for bulk material handling.
Suitable for extraction under silos, dosing, or transfer up to 10 meters, the electromechanical vibrating conveyor is the most versatile solution for all bulk handling industries.
Maintenance is facilitated by the absence of moving parts in contact with the product and the use of reliable vibrating motors, ensuring maximum availability.
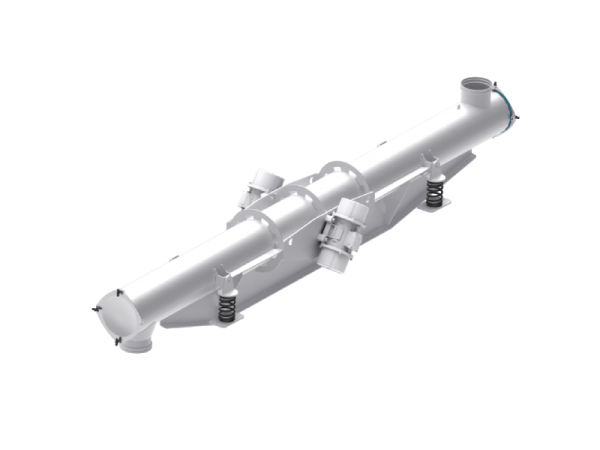
Vibrating High Hygiene Tubular Conveyor
Specifically designed for food and agro-food applications, the High Hygiene Tubular Vibrating Conveyor combines the benefits of vibratory conveying (no creation of fines, no pressure on the product, and no mechanical parts in contact with the product) with confined conveying, inside a tube with no retention zones and a surface finish compliant with food industry standards.
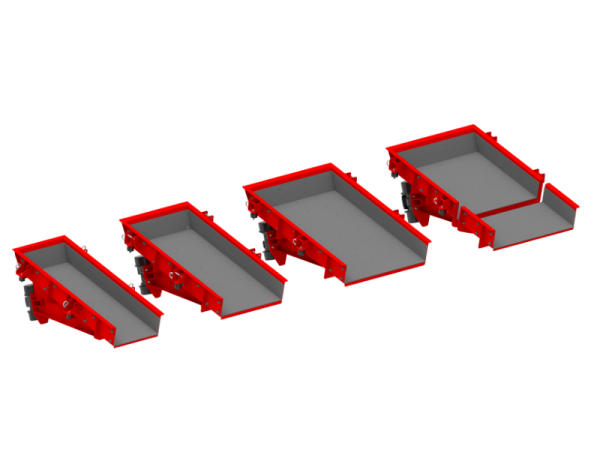
Quarry Range - Electromechanical Vibrating Conveyors
Vibrating conveyors/extractors specially designed for quarry applications.
This specific range meets the demands of mineral extraction by optimizing the design and power to achieve the best performance/price ratio without compromising reliability.
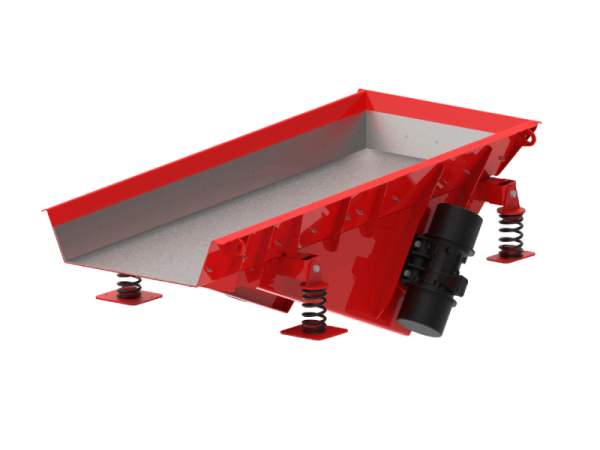
Extractor / Conveyor EME
Vibration conveying limits abrasion, prevents the creation of fines (no mechanical constraints on the product), and ensures a constant and controlled volumetric flow.
Suitable for extraction under silos, dosing, or transfer up to 10 meters, the electromechanical vibrating conveyor is the most versatile solution for all bulk handling industries.
Maintenance is facilitated by the absence of moving parts in contact with the product and the use of vibrating motors, ensuring maximum availability.